The uncomfortable economics of an off – spec shipment after thousands of tonnes have already arrived
The vessel has sailed thousands of kilometres.
Freight has been paid. The cargo has reached port. Thousands of tonnes of coal, coke, pellets, scrap or another raw material are waiting to be discharged or may already be sitting in the stockyard.
Then the laboratory report arrives.
The material is off – spec.
Perhaps coal ash is higher than contracted. Coke contains more fines than expected. Pellet size distribution has deteriorated. Scrap contains excessive contamination. Pig iron chemistry is outside the agreed range.
On paper, the solution sounds simple: reject the material.
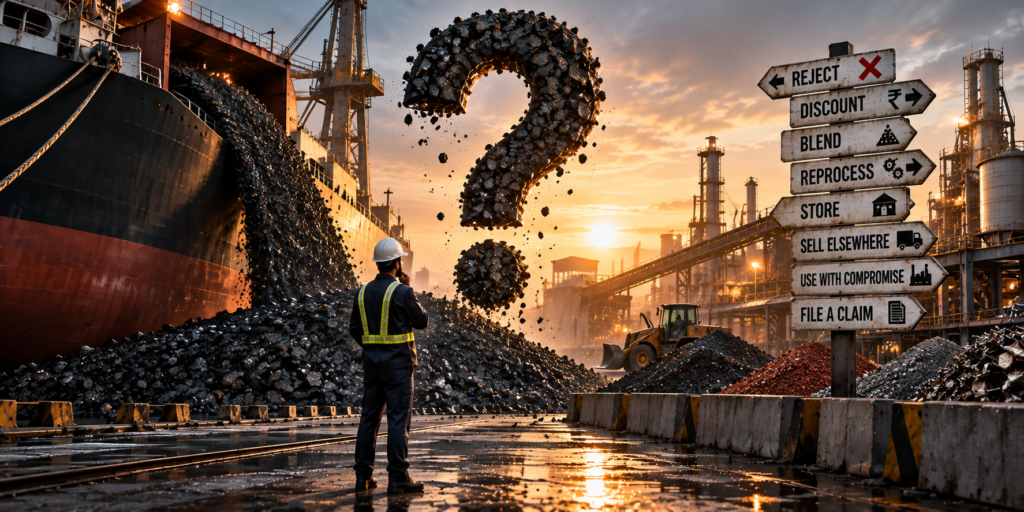
In reality, once 20,000, 40,000 or 60,000 tonnes have physically arrived, rejection can become one of the most complicated decisions in raw-material procurement.
Because an off – spec cargo does not disappear when the laboratory says “failed.”
- Someone still owns it.
- Someone has financed it.
- Someone has to store it.
And eventually, somebody has to decide what to do with it.
The First Question Is Not “Is It Off-Spec?”
The first question is :
How far off-spec is it and what does that actually mean for the plant?
There is an enormous difference between a shipment that marginally misses one contractual parameter and material that is fundamentally unsuitable for the intended process.
Suppose coal was contracted at a maximum 10% ash but testing establishes 11%.
That extra percentage point represents 500 tonnes of additional ash in a 50,000 – tonne cargo, assuming the figures are being compared on the same analytical basis.
That is not insignificant.
But it also does not automatically mean the entire cargo is unusable.
The plant needs to understand whether the deviation can be absorbed operationally, whether the material can be blended with better coal, whether compensation makes the economics acceptable and whether using it introduces additional costs elsewhere.
The specification identifies the deviation.
The plant has to calculate the consequence.
Rejecting 50,000 Tonnes Is Much Easier in an Email Than at a Port
Before loading, rejecting unsuitable material can be relatively straightforward.
After arrival, everything changes.
If a steel plant refuses a cargo, the material still occupies physical space. A vessel may be waiting. Port charges may accumulate. Storage costs can increase. The seller may need to locate another buyer. Additional transport may be required.
If the cargo has already been discharged and mixed with other inventory, the situation becomes even more difficult.
This is why commercial contracts normally contain detailed provisions governing quality, sampling, inspection, tolerances, claims and dispute resolution.
The critical question becomes whether the deviation legally and commercially allows outright rejection or whether the agreed remedy is a price adjustment, quality penalty or another form of settlement.
A “failed” laboratory result and a legally rejectable cargo are not always the same thing.
Sometimes the Cheapest Solution Is to Keep the Bad Cargo
That sounds counterintuitive, but steel economics frequently works this way.
Imagine a 40,000 – tonne shipment is slightly below specification.
Rejecting it may involve storage, additional freight, contractual disputes, replacement procurement and production risk.
The supplier instead offers a discount of ₹700 per tonne.
That represents ₹2.8 crore across the cargo.
Now the steelmaker has a calculation to make.
Will the off spec material create more or less than ₹2.8 crore of additional operational cost?
If blending, additional handling, lower yield or increased fuel consumption costs only ₹1.5 crore, accepting the discounted cargo may make economic sense.
If the process penalty is ₹5 crore, the discount is inadequate.
This is why an off spec claim should never be negotiated only around the purchase price.
The correct number is the cost of using the deviation.
Blending Is Often the Steel Plant’s Escape Route
One of the most powerful tools available to steelmakers is blending.
Suppose a coal cargo arrives with 13% ash when the desired blend needs to be around 10%.
The plant may combine it with lower-ash coal so that the final blend remains within an operationally acceptable range.
Similarly, an iron-bearing material with one undesirable characteristic may sometimes be combined with a stronger material to stabilise the overall burden.
This effectively converts a cargo problem into a blending problem.
But blending is not magic.
The plant needs enough corrective material. Stockyards must be able to segregate and reclaim accurately. The chemistry and physical characteristics of both materials must be understood.
Most importantly, the economics must still work.
Using premium material to compensate for cheaper off-spec material can destroy the original saving.
The real calculation is therefore not :
Can we blend it?
It is :
What will it cost us to blend it successfully?
Reprocessing Can Rescue Value But It Isn’t Free
Some off – spec materials can be improved physically.
Oversized material may be crushed.
Excess fines may be screened.
Scrap can be sorted and contaminants removed.
Certain materials can be dried or otherwise processed depending on the problem and available infrastructure.
But every additional processing stage introduces cost.
- Equipment is required.
- Labour is required.
- Energy may be consumed.
- Handling losses occur.
- Time is lost.
And the material may need to be moved multiple times before it finally becomes usable.
Consider 20,000 tonnes of scrap requiring additional sorting at an illustrative ₹500 per tonne.
That is already ₹1 crore of extra processing cost before accounting for material removed during sorting or production delays.
An off – spec cargo may therefore be technically recoverable while remaining commercially unattractive.
Storage Turns Quality Problems Into Financial Problems
Sometimes the plant cannot use the material immediately but does not want to reject it.
So it stores it.
That sounds harmless.
It isn’t.
Raw – material inventory ties up working capital. Storage occupies valuable stockyard capacity. Material may need segregation to prevent accidental mixing. Some materials can deteriorate or become more difficult to handle over time.
There is also an opportunity cost.
If an off – spec cargo occupies 10,000 tonnes of limited covered storage, that space may no longer be available for better material.
At a port, storage and demurrage – related exposure can become even more serious depending on contractual arrangements and how quickly the problem is resolved.
An unresolved quality dispute therefore has a clock attached to it.
Every additional day can change the economics.
Then Begins the Claim
When the buyer and seller disagree about quality, sampling becomes enormously important.
- Was the sample representative?
- Where was it taken?
- Who supervised sampling?
- Which laboratory tested it?
- Which analytical standard was used?
- Was moisture measured on the correct basis?
- Were samples collected at loading or discharge?
- Could segregation have occurred during transport?
A 50,000 – tonne cargo may ultimately be represented commercially by a comparatively tiny laboratory sample.
That makes sampling integrity critical.
If the buyer reports 12% ash and the seller reports 10.5%, the disagreement is not merely 1.5 percentage points.
It can represent hundreds of tonnes of unwanted mineral matter and potentially a very large commercial claim.
This is why independent inspection, sealed reference samples and clearly defined testing procedures matter so much.
They are not paperwork.
They are protection against disputes worth crores.
Alternative Buyers Can Become the Exit Door
One plant’s unusable material may be another plant’s acceptable feedstock.
Steel plants operate different furnaces, products, burden strategies and quality requirements.
Coal unsuitable for one industrial process may have value in another application.
Scrap rejected by a producer of demanding steel grades may be acceptable to a plant producing a more tolerant product.
A pellet or iron – bearing material that does not fit one burden strategy may fit another.
This creates an important role for traders.
A trader with a broad market network may be able to redirect off-spec material toward a customer whose process can tolerate the specification.
The cargo has not magically improved.
Its fit has changed.
That distinction matters enormously in commodity trading.
Raw-material quality is not always simply “good” or “bad.”
Often it is suitable or unsuitable for a particular user.
The Most Dangerous Option Is the Operational Compromise
Sometimes the cargo is accepted because the plant urgently needs material.
Inventory is low.
A replacement cargo will take weeks.
Production cannot stop.
The plant therefore uses material it would normally avoid.
This is where an apparently commercial decision can become an operational one.
Coal quality changes and the fuel blend needs adjustment.
Additional coke fines alter handling.
Pellet quality changes the burden.
Scrap contamination requires charge modifications.
Pig iron chemistry forces additional refining.
The furnace team starts compensating for a decision made somewhere else in the supply chain.
And compensation has a cost.
- More fuel.
- More flux.
- More energy.
- More slag.
- More processing.
- Lower productivity.
- Additional testing.
- Potentially lower yield.
The plant may have “saved” itself from a supply shortage while quietly transferring the cost into operations.
The Cheapest Settlement Is Not Always the Best Settlement
Suppose a supplier offers ₹1 crore to settle an off-spec claim.
That number sounds attractive.
But the plant should ask what the material actually cost it.
Perhaps additional processing cost ₹30 lakh.
Blending required ₹25 lakh of higher – quality material.
Lower yield cost another ₹20 lakh.
Storage and handling added ₹10 lakh.
Production inefficiency contributed another ₹40 lakh.
The total consequence is now ₹1.25 crore.
The ₹1 crore settlement did not make the plant whole.
This is why sophisticated quality claims increasingly require input from procurement, laboratory teams, operations, logistics and finance.
The commercial department sees the discount.
Operations sees the consequence.
Both numbers belong in the same calculation.
The Best Off – Spec Strategy Starts Before the Ship Sails
The most effective way to manage an unwanted cargo is to prevent it from becoming unwanted in the first place.
That means clear specifications.
- Representative pre – shipment sampling.
- Reliable laboratories.
- Supplier performance history.
- Defined tolerance limits.
- Agreed inspection procedures.
- Clear claim mechanisms.
Understanding how much deviation the plant can genuinely absorb.
And, importantly, knowing which alternative markets could take the material if something goes wrong.
Supplier evaluation should therefore include more than average quality.
It should also ask :
- What happens when the supplier gets it wrong?
- Does the supplier respond quickly?
- Does it accept independent testing?
- Does it settle claims fairly?
- Can replacement material be arranged?
A supplier’s behaviour during a bad cargo can reveal more about the relationship than twenty perfect shipments.
An Off – Spec Cargo Is Not a Quality Problem. It Is a Decision Problem.
Once thousands of tonnes have arrived, there is rarely one perfect answer.
- Rejecting the cargo costs money.
- Accepting it can cost money.
- Blending costs money.
- Reprocessing costs money.
- Storing it costs money.
Selling it elsewhere may require a discount.
And forcing it through the plant can transfer the problem directly into production.
The correct decision depends on which option creates the lowest total economic and operational consequence.
That is why raw – material procurement does not end when the cargo reaches the gate.
Sometimes that is exactly where the hardest part begins.